


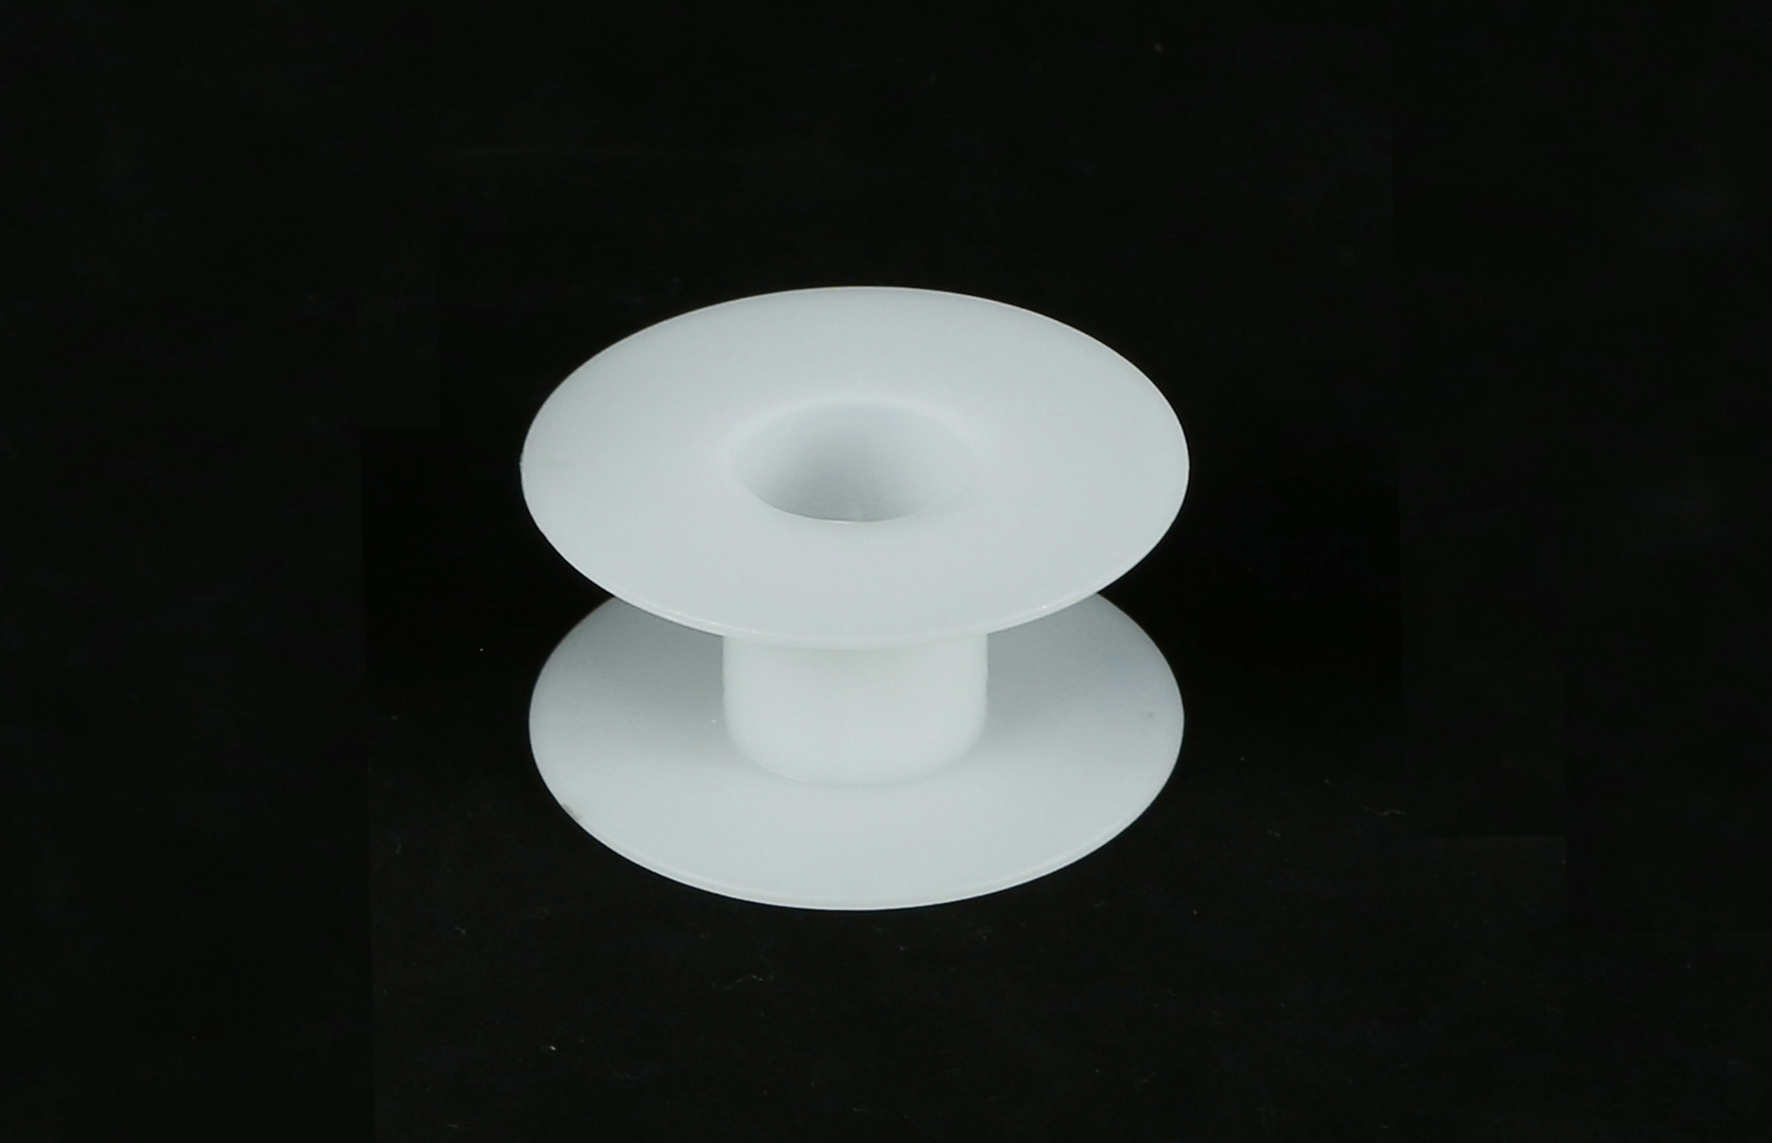
Plastic spool process requirements
Plastic spools undergo many processes of control and inspection from the start of production. To manufacture a high-quality plastic spool, it is necessary to control the process conditions such as temperature, pressure, and speed, in order to achieve a product that is free of surface defects, has stable weight, and is free of internal stress. During the production process, the temperature, pressure, and speed should not fluctuate too much.
2022-02-04

Plastic spoolFrom the start of production, many processes of control and inspection will be experienced. To manufacture a high-quality plastic spool, it is necessary to control the process conditions such as temperature, pressure, and speed, to achieve the goals of no surface defects, stable weight, and no internal stress. During the production process, temperature, pressure, and speed should not fluctuate too much.
Plastic spool process requirements:
1. Drying of raw materials: The moisture content of ABS should be controlled below 0.3%. The drying conditions for the hopper dryer used in the injection molding machine are: before starting, in dry winter, dry at 75-80°C for 2-3 hours, and in summer rainy days, dry at 80-90°C for 4-8 hours.
2. Temperature control: To prevent the spool from being affected by environmental temperature, the mold should use a constant temperature machine to control the temperature, generally keeping the mold temperature at 70-80°C. After ABS reaches the plasticizing temperature, the increase in temperature leads to a very small decrease in melt viscosity. If the temperature continues to rise blindly, it will cause thermal degradation of ABS, which has low heat resistance, and instead increase the melt viscosity, making injection more difficult. Therefore, the temperature of the barrel and nozzle is generally controlled at 200-230°C. The temperature of the first section of the barrel and the nozzle should be lower than that of the second and third sections of the barrel.
3. Pressure control: The viscosity of the ABS melt is relatively high, and the shape of the spool is cylindrical, so a higher injection pressure is used during injection; otherwise, the product is not easy to fill or the weld marks are particularly stubborn. The longer the barrel, the greater the injection pressure, while also adjusting the holding pressure and holding time. However, injection pressure should not be increased blindly. When the pressure is too high, the product condenses quickly under high pressure, resulting in high residual stress, which lowers the strength of the spool and is prone to flash, also causing greater wear on the injection machine and mold.

4. Speed control: The injection should be mainly at medium speed.
5. Time control: The cooling time should be based on the product being able to be completely removed without deformation, while also considering the control of the product's fit dimensions.
6. Weight and size control: Under certain mold conditions, fine-tune the holding pressure and time. When the weight is too light or the tolerance is too small, increase the holding pressure and extend the holding time; conversely, decrease the holding pressure and shorten the holding time.
The above is aboutPlastic spoolthe relevant content sharing of process requirements. In summary, when starting up or changing raw materials, it is necessary to strengthen the monitoring frequency of the spool's weight and dimensions. Only after the weight and dimensions stabilize can continuous production be carried out, while also conducting random inspections as required. Only when temperature, pressure, speed, and time reach a dynamic balance can qualified products be produced.
Contact Us
Mailbox:
wangyumei630@163.com
Tel:
086-769-85707005
Mobile:
086 132 6843 4928
Address:
Building 3, Wanshan Factory, No. 38 Hulin Road, Humen Town, Dongguan City
CONTACT US
ZhenHua Packing Machinery
Tel: 086-769-85707005
Mobile: 086 132 6843 4928
Email: wangyumei630@163.com
Address: Building 3, Wanshan Factory, No. 38 Hulin Road, Humen Town, Dongguan City
ZhenHua Packing Machinery
Follow our media for more information
Online message
If you are interested in our products, please leave your contact information
SAF Coolest v1.3 设置面板 GAGSE-ZGYF-JASXE-ZXE
无数据提示
Sorry, the current column has no content for the time being.!
You can view other columns or returnHome Page